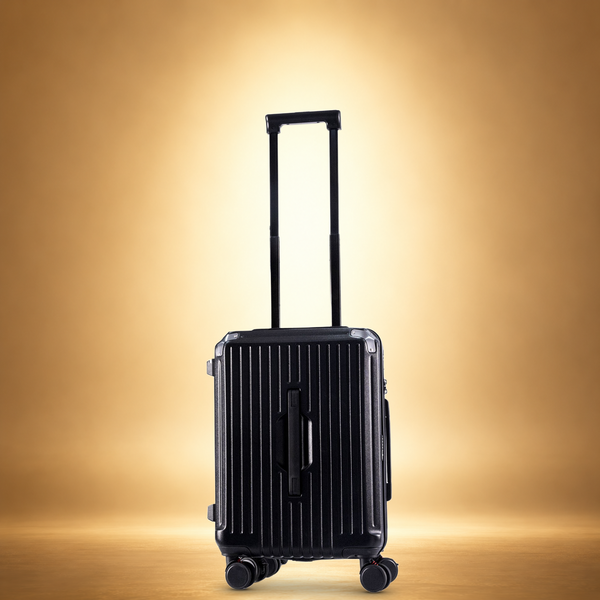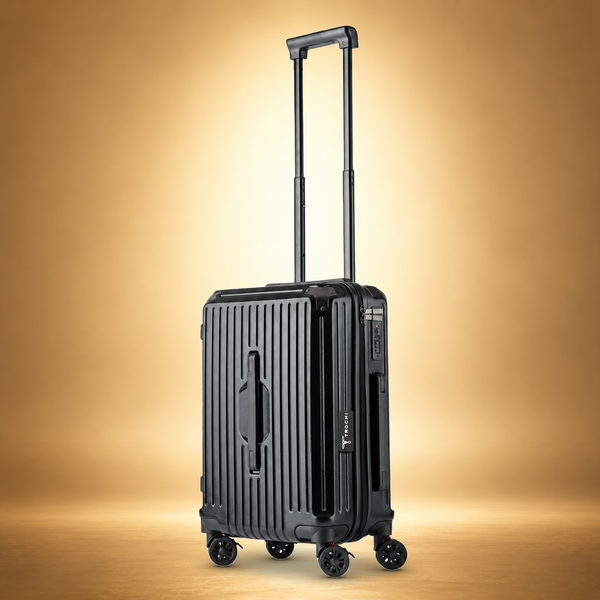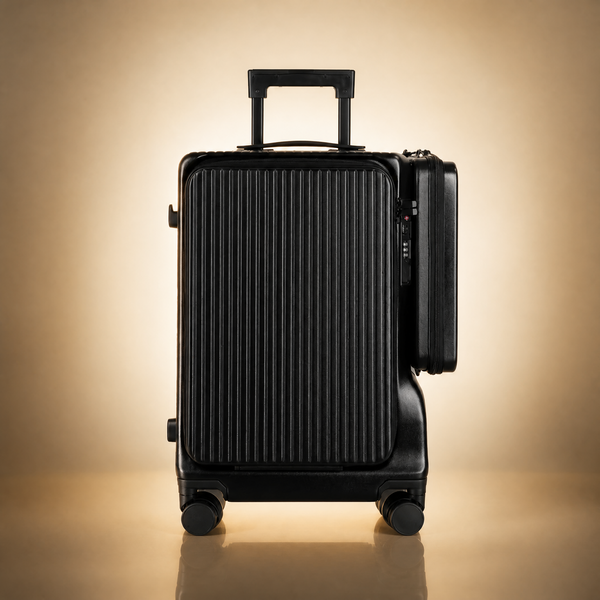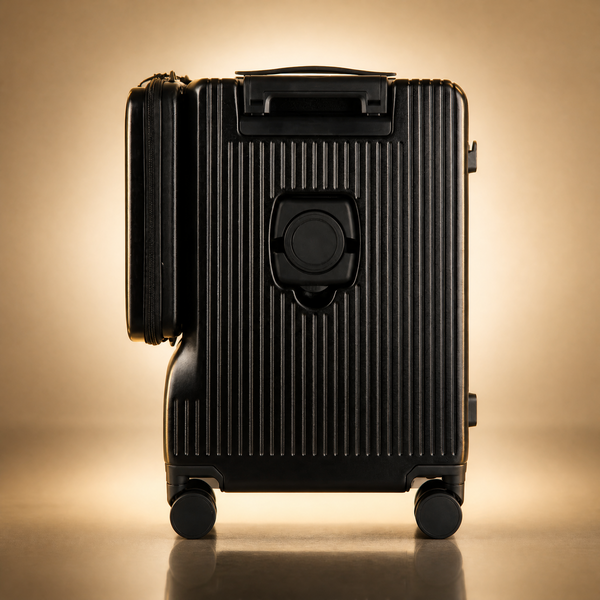
How it's made

A lot goes into a case that is meant to last a lifetime of departures. This is what goes in.

See how it is made


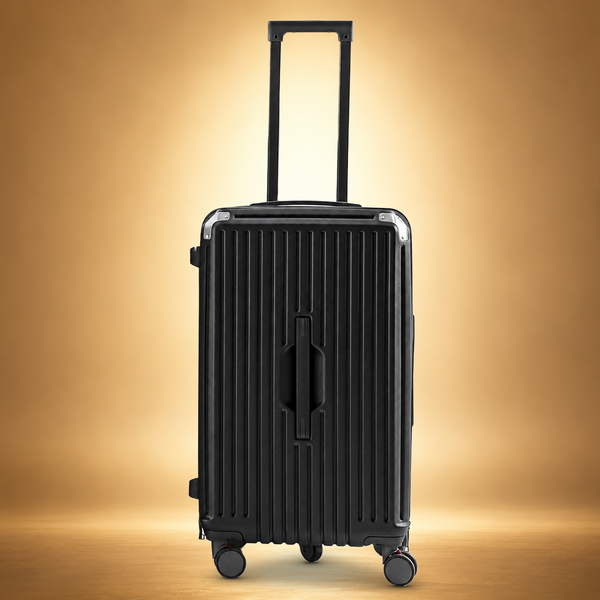
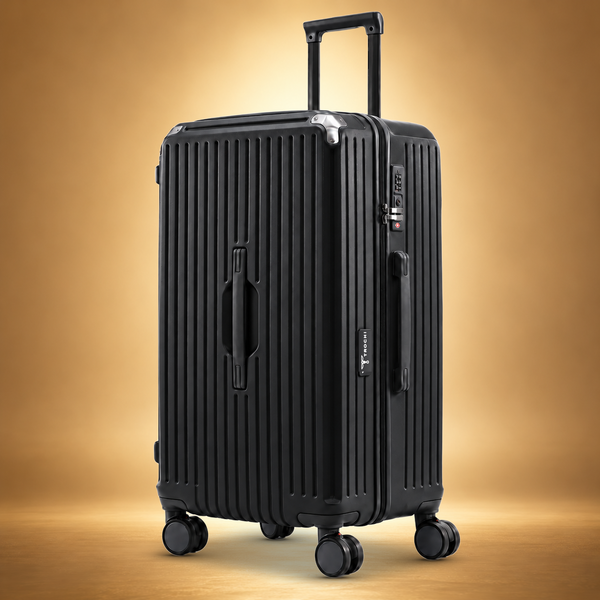
We spent two years and eleven prototypes on the parts no one photographs.

Wheel bearings. Handle stops. The rivet under the corner guard. A great suitcase is decided in the places you will never look, so that is where we spent the time.

How it is made

From sheet to suitcase, in twelve steps.

Shell, lining, hardware and assembly happen under one roof. Nothing is outsourced across three suppliers and stapled together at the end. These are the steps, filmed on our line.

  1. 01 Raw material and sheet
  2. 02 Shell forming
  3. 03 CNC trimming
  4. 04 One factory. Every case.
  5. 05 Lining and straps, sewn
  6. 06 Riveted, not glued
  7. 07 Handles and components
  8. 08 Lining fitted by hand
  9. 09 Edge stitching
  10. 10 Finishing and inspection
  11. 11 The overhead line
  12. 12 Bagged and boxed

01 Materials

Raw material and sheet

It starts as polycarbonate and coloured sheet stock, kept on the floor until the line calls for it. We use 100% virgin polycarbonate, not regrind. Regrind is cheaper, and it is also how a shell cracks in a cold cargo hold.

02 箱壳

Shell forming

Each half-shell is pressed in its mould, released and lifted out, then racked and left to settle before anything is cut.

03 箱壳

CNC trimming

A CNC machine follows the same path around every shell edge and cuts the openings, so the frame, zipper track and lid meet flush on every case.

04 Factory

One factory. Every case.

Shell storage and the sewing floor sit under one roof. Every TROCHI case is built on the same line by the same team, which is the only way the tenth case matches the first.

05 Lining

Lining and straps, sewn

Lining panels, compression straps and binding are machine-sewn and cut for one shell size.

06 Hardware

Riveted, not glued

Corner guards, feet, handle mounts and wheel housings are riveted through the shell. Glue is faster on the line, and it is also the first thing to let go after a conveyor belt.

07 Assembly

Handles and components

Handles and hardware are prepared at the bench and assembled onto the case. The telescopic handle is an alloy assembly that locks at three heights.

08 Lining

Lining fitted by hand

The sewn lining goes into the shell and is smoothed and positioned by hand.

09 Assembly

Edge stitching

The case edge is stitched and joined all the way round.

10 Inspection

Finishing and inspection

The lining is pressed, details are finished, and every case is opened, closed and checked by hand.

11 Factory

The overhead line

Finished cases travel the overhead conveyor to final inspection and packing.

12 Packing

Bagged and boxed

Each case is bagged, boxed and sealed at the end of the line.

Next


Then we try to break it.

Wheel running, handle shock, telescopic handle cycling and drop tests, filmed on the rigs our cases go through.

See the quality check